CCUS
Providing solutions for CO₂ capture, separation, purification, liquefaction, and resource utilization to support the green and low-carbon transformation of industry.
Separation
Relying on membrane separation, adsorption separation, and cryogenic separation technologies, CO₂ and multi-component resources are efficiently separated from multi-source gases such as natural gas and biogas.
Purify
Multi-stage purification process deeply purifies CO₂ purity up to 99.99% mol+, with methane purity simultaneously improved.
Liquefaction
Supporting low-temperature distillation and liquefaction processes to achieve high-efficiency CO₂ liquefaction, supporting the implementation of CCUS and resource utilization.
Utilization
Synergistically extracting high-value components such as helium, hydrogen, and NGL, widely used in green energy and industrial gases.
Customized gas recovery and purification
Methanol catalytic reforming hydrogen production process mixes methanol and water in specific proportions and sends it into a reforming reactor equipped with a high-performance catalyst. Under suitable temperature and pressure conditions, methanol undergoes a series of complex chemical reactions, decomposing into gases such as hydrogen and carbon dioxide. Subsequently, through a precise purification system, impurity gases are removed, ultimately producing high-purity hydrogen gas with purity exceeding 99.99%, meeting stringent usage requirements.
Efficient hydrogen productionRapid startupCosts are controllableSafe and reliableRemote control
99.99%
The purity is reachable
Carbon dioxide separation and utilization
Deeply cultivating diverse core technologies such as membrane separation, adsorption separation, cryogenic separation, and distillation, it specializes in creating integrated solutions for carbon dioxide capture, purification, liquefaction, and resource utilization. These solutions are widely applied in natural gas purification, chemical tail gas treatment, biogas refining, CCUS, and other fields, supporting the implementation of dual carbon goals and promoting the development of green circular industries.
Efficient separationLow energy consumptionHigh purityModular designResource utilization
99.99% mol+
CO₂ purity is achieved
95%+
CO₂ recovery rates can be achieved
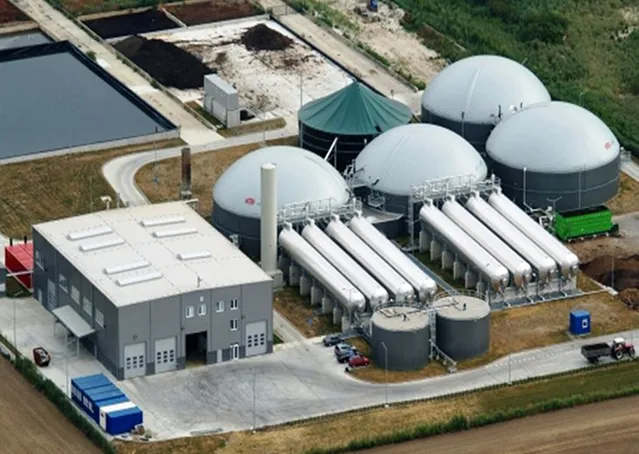
Biogas separation, purification, and liquefaction
With core processes such as membrane separation, PSA, cryogenic separation, and liquefaction, we specialize in providing solutions for biogas purification, biogas preparation, and CO₂ separation and liquefaction. We efficiently separate and purify methane from biogas, promoting the high-value application of biomethane, and are widely used in green energy, industrial fuels, distributed energy, and other fields.
Efficient purificationLow energy consumptionResource utilizationModular designGreen and low-carbon
99.99% mol+
Methane purity can be achieved
99.99% mol+
Methane recovery rates can be achieved
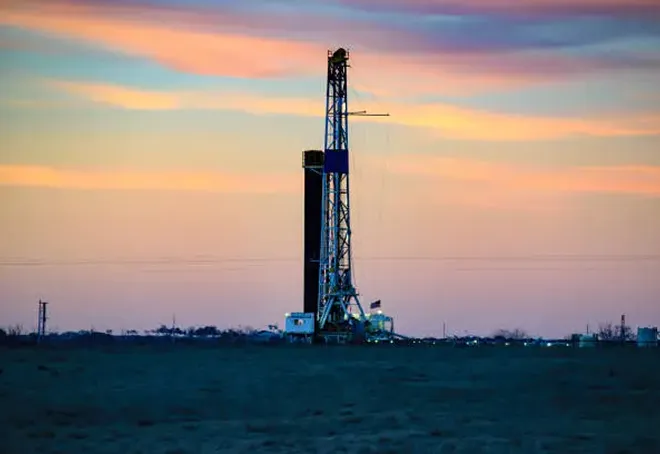
Multi-component separation and comprehensive utilization of natural gas / shale gas / coalbed methane
With core technologies in membrane separation, PSA, cryogenic separation, and distillation, we specialize in providing separation, purification, and comprehensive utilization solutions for multi-component gases (helium, hydrogen, carbon dioxide, natural gas condensate NGL, etc.) in natural gas, shale gas, and coalbed methane, achieving efficient resource development and high-value utilization.
Multi-component coordinated separationEfficient resource utilizationModular designCustomized solutions
99.9999% mol+
The product gas purity can be achieved
95%+
The target component recovery rate can be achieved
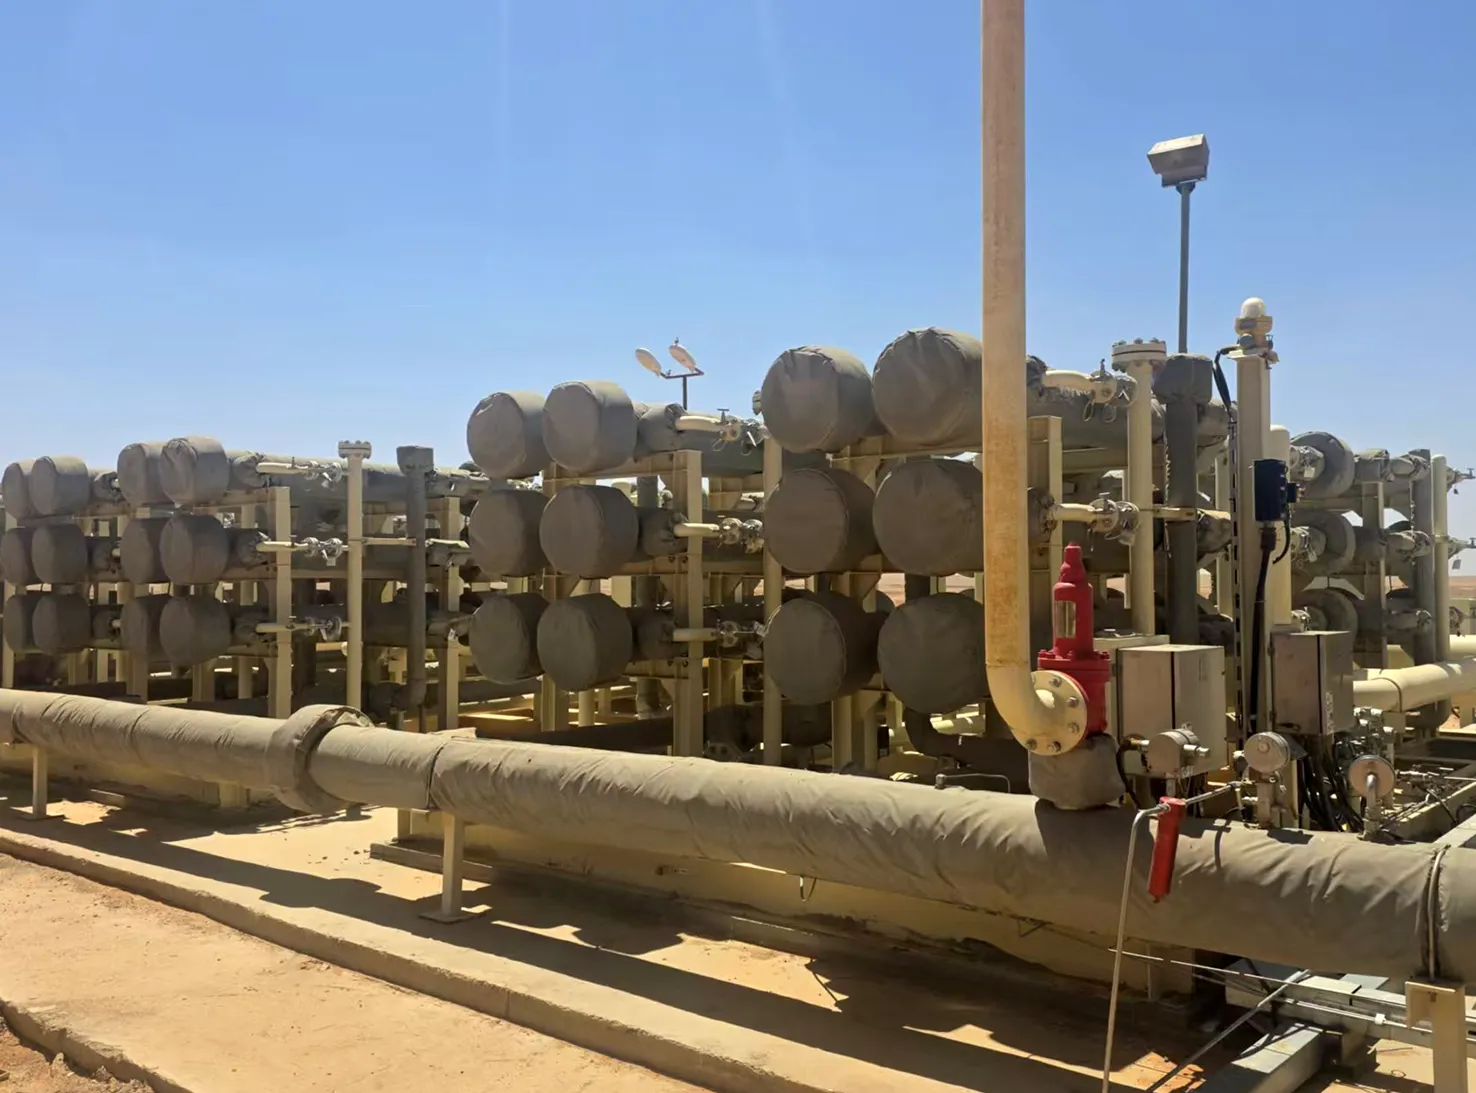
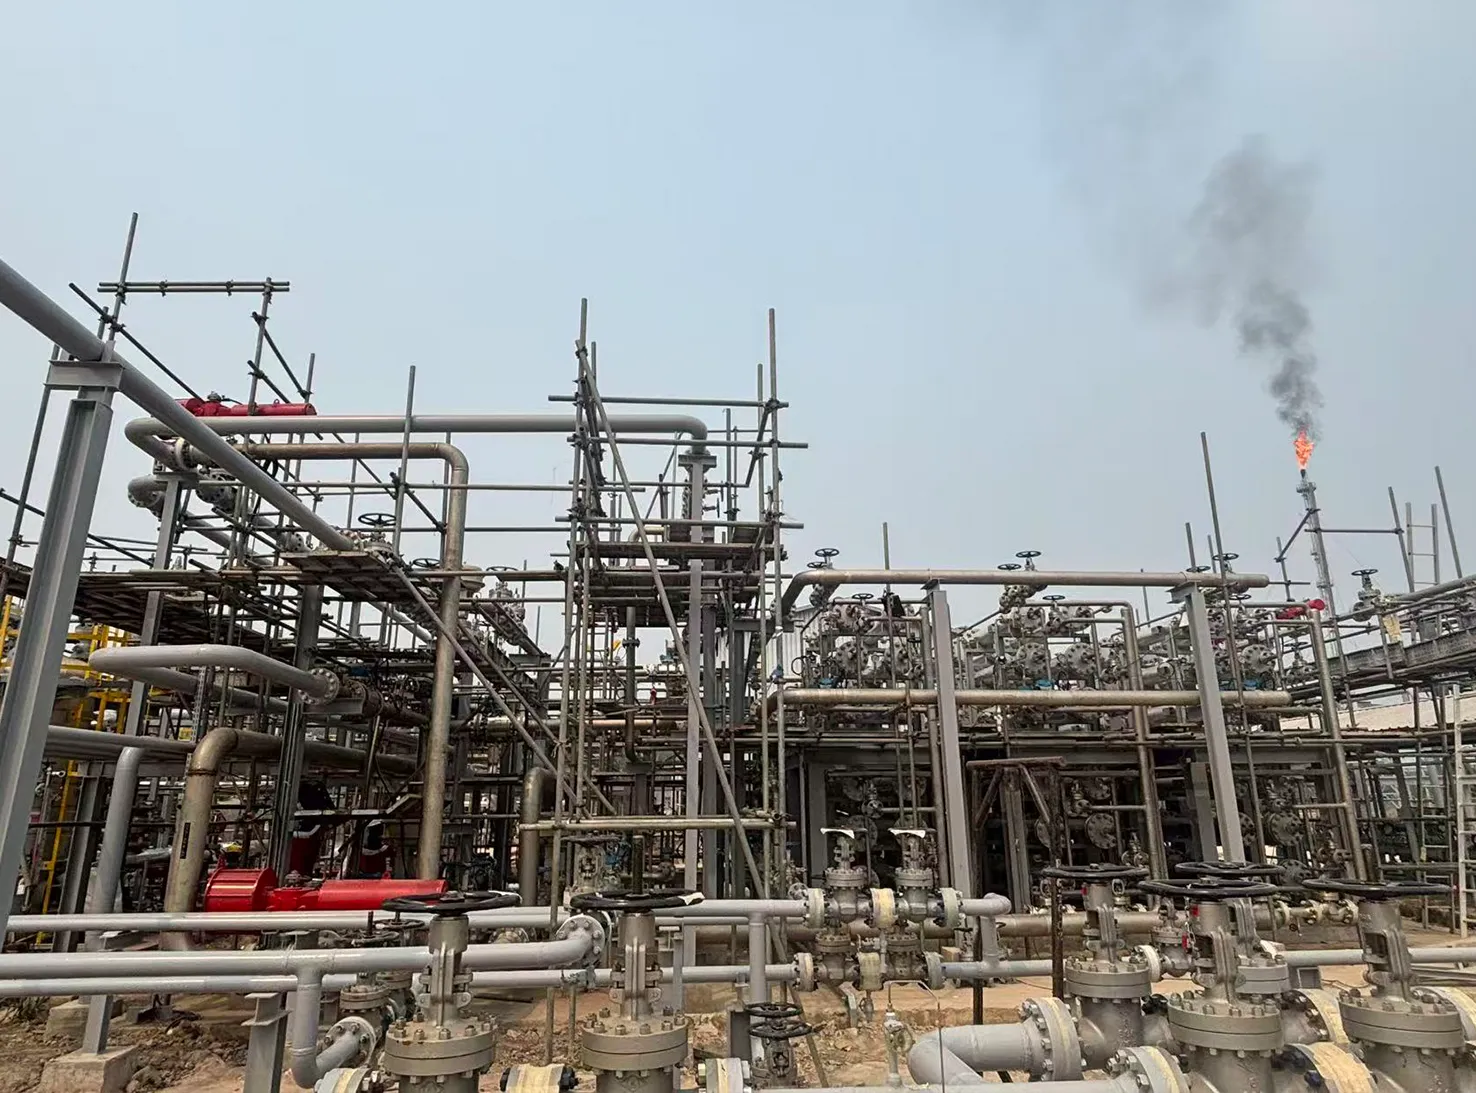
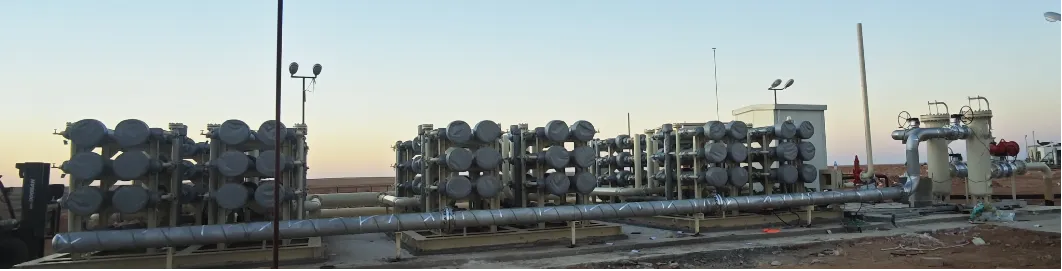
Track Record
Real-world applications of RefineTek technology across industries.